
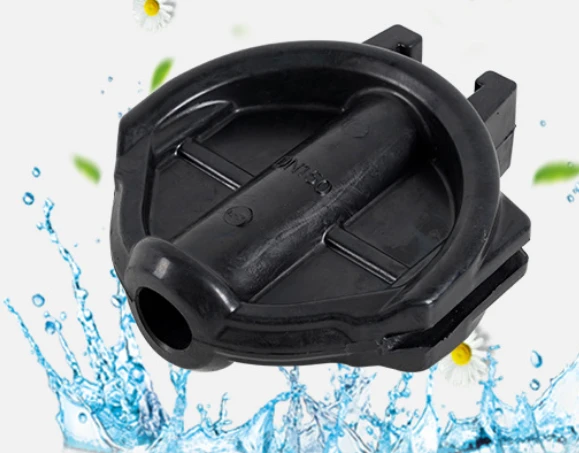


Hangzhou Bright Rubber Plastic Product Co., Ltd. is one of the leading manufacturers and suppliers of industrial rubber valve in China. If you're going to buy industrial rubber valve made in China, welcome to get more information from our factory. We also accept customized orders.
Industrial Rubber Valve
Product Characteristic
| Available Materials |
NR, NBR, EPDM, HNBR, CR, PU, Silicone, FKM, IIR |
| Core Function | Fluid sealing, pipeline isolation, pressure buffering |
| Hardness Range | 20‑90 Shore A (customizable), soft-to-medium flexible formulas |
|
Structural Feature |
Precision molded, tight sealing tolerance |
| Working Temperature | -60°C to +230°C (material matched) |
|
Performance Strength |
Leak-proof, durable, medium-resistant |
| Main Applications | Food processing equipment, medical devices, high-temperature machinery |
| Industrial Adaptation | Water, oil, gas, chemical fluid systems |
| Batch Stability | Uniform texture, consistent sealing performance |
| Shape and Size | OEM according to drawings |
| Payment Term | L/C, T/T, WEST UNION, PAYPAL, ESCROW |
| Quality certification | RoHS, REACH, FDA (food-grade grades), etc. |
Product Introduction
This full-series industrial rubber valve portfolio is professionally developed for industrial pipeline switching, fluid sealing and pressure isolation applications. Different from general rubber accessories, these rubber valve parts focus on dynamic sealing stability and medium adaptability, ensuring zero leakage during repeated opening, closing and pressure fluctuation cycles.
We configure exclusive material solutions for different working environments, covering conventional civil pipelines, oily mechanical systems, outdoor weather-exposed equipment, high-temperature production lines, corrosive chemical media and high-precision sealed units. All raw rubber materials are strictly screened and vulcanized with standardized processes, ensuring excellent compression resilience, surface finish and structural stability of each valve rubber part.
Material Adaptation & Core Advantages
NR Rubber: Features ultra-high elasticity and excellent compression recovery, ideal for conventional water pipeline and general-pressure valve sealing, delivering smooth opening and closing feedback.
NBR Rubber: Optimized for oil-based medium environments, with stable anti-swelling performance, perfectly suited for fuel and hydraulic system valve accessories.
EPDM Rubber: Boasts outstanding weather and aging stability, maintaining long-term reliable sealing for outdoor pipelines, steam and water circulation valve systems.
HNBR Rubber: Adopts an upgraded hydrogenated formula, with enhanced high-temperature and fatigue resistance, suitable for high-cycle continuous working industrial valve equipment.
CR Neoprene: Provides balanced flame retardant and moisture-resistant performance, adapting to humid workshop and ventilation pipeline valve systems.
PU Polyurethane: Delivers superior wear resistance and structural rigidity, ideal for frequently opened and closed heavy-duty mechanical valve components.
Silicone Rubber: Features extreme temperature adaptability and hygienic performance, widely used in food, medical, and high- and low-temperature circulating valve systems.
FKM Fluororubber: Offers top-tier chemical and high-temperature resistance, stable and durable in strong acid, alkali, and special chemical fluid valve working conditions.
IIR Butyl Rubber: Possesses ultra-low air permeability and excellent tightness, perfect for vacuum equipment and high-airtight requirement valve sealing systems.
Application Scenarios
The full-material rubber valve series is widely applicable to municipal water supply and drainage pipelines, industrial hydraulic systems, chemical fluid transmission lines, outdoor ventilation equipment, food and pharmaceutical processing pipelines, vacuum precision equipment, and high-temperature industrial circulating systems. It effectively ensures pipeline sealing safety, stabilizes internal fluid pressure, and extends the service cycle of the overall valve system.
Customization & Supply Support
We provide one-stop customized services for all rubber valve accessories. According to the customer's medium type, working temperature, pressure grade, and installation size, we select matching rubber materials and optimize structural design. Support pre-production sample verification, small-batch trial orders, and large-scale stable bulk supply, serving global industrial equipment manufacturers and pipeline engineering projects.
Company Information


Hot Tags: industrial rubber valve, china, manufacturers, suppliers, factory, customized, made in China, Anti Vibration Feet Damper For Machinery, Compression Molded Natural Rubber Bumper, Natural Rubber Vibration Damper For Car, Standard Natural Rubber Silent Block, Type A Rubber Vibration Dampers, Type B Rubber Vibration Dampers


